Where does the wrap start to lift?
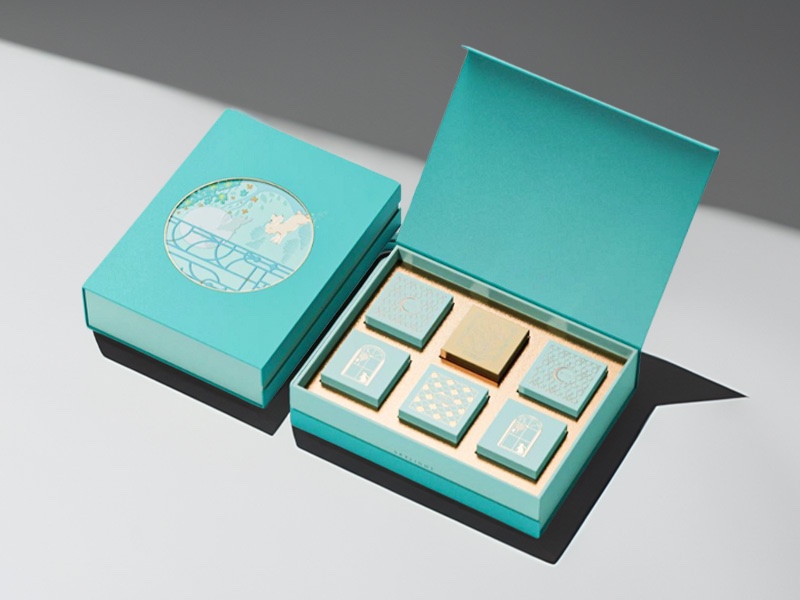
M-6123 and M-6192 belong to the rigid box family with 55±2% solids and a stated viscosity of 800–5,000 mPa·s. Photograph the face, corners and turn-ins, noting where lifting first appears. A loose corner at the forming station and a bowed lid after storage require different comparisons of application, forming and drying.
Which conditions belong in the trial record?
Record the wrap finish, greyboard, dimensions, adhesive feed and forming sequence before a rigid box trial. M-6123–M-6328 grades list diaphragm-pump or hopper feeding and a 48-hour cure reference. Note coating transfer, time before wrapping and pressing, then keep one labelled box per condition to compare staining, corner lift and panel movement.
- Wrap and board
- Give the wrap stock and finish, the greyboard thickness, and the box dimensions. Identify any film or varnish on the bonding face.
- Glue and forming
- Describe the glue feed, applicator, time from coating to wrapping and the pressing sequence.
- Appearance over time
- Keep one box from each trial. Note the time, storage conditions and any bubbles, corner lift, staining or panel bow.
How should the trial be compared with current production?
Compare the candidate rigid box grade on wrap and board from the same batches. Inspect registration after forming and record edge lift and panel flatness after the agreed conditioning. The family’s at least 95% fiber-tear benchmark needs a defined construction and method; it does not replace appearance checks on a soft-touch finished box.